







11th September 2026
When Should You Switch to Progressive Die Stamping A Prototype-to-Production Cost Guide
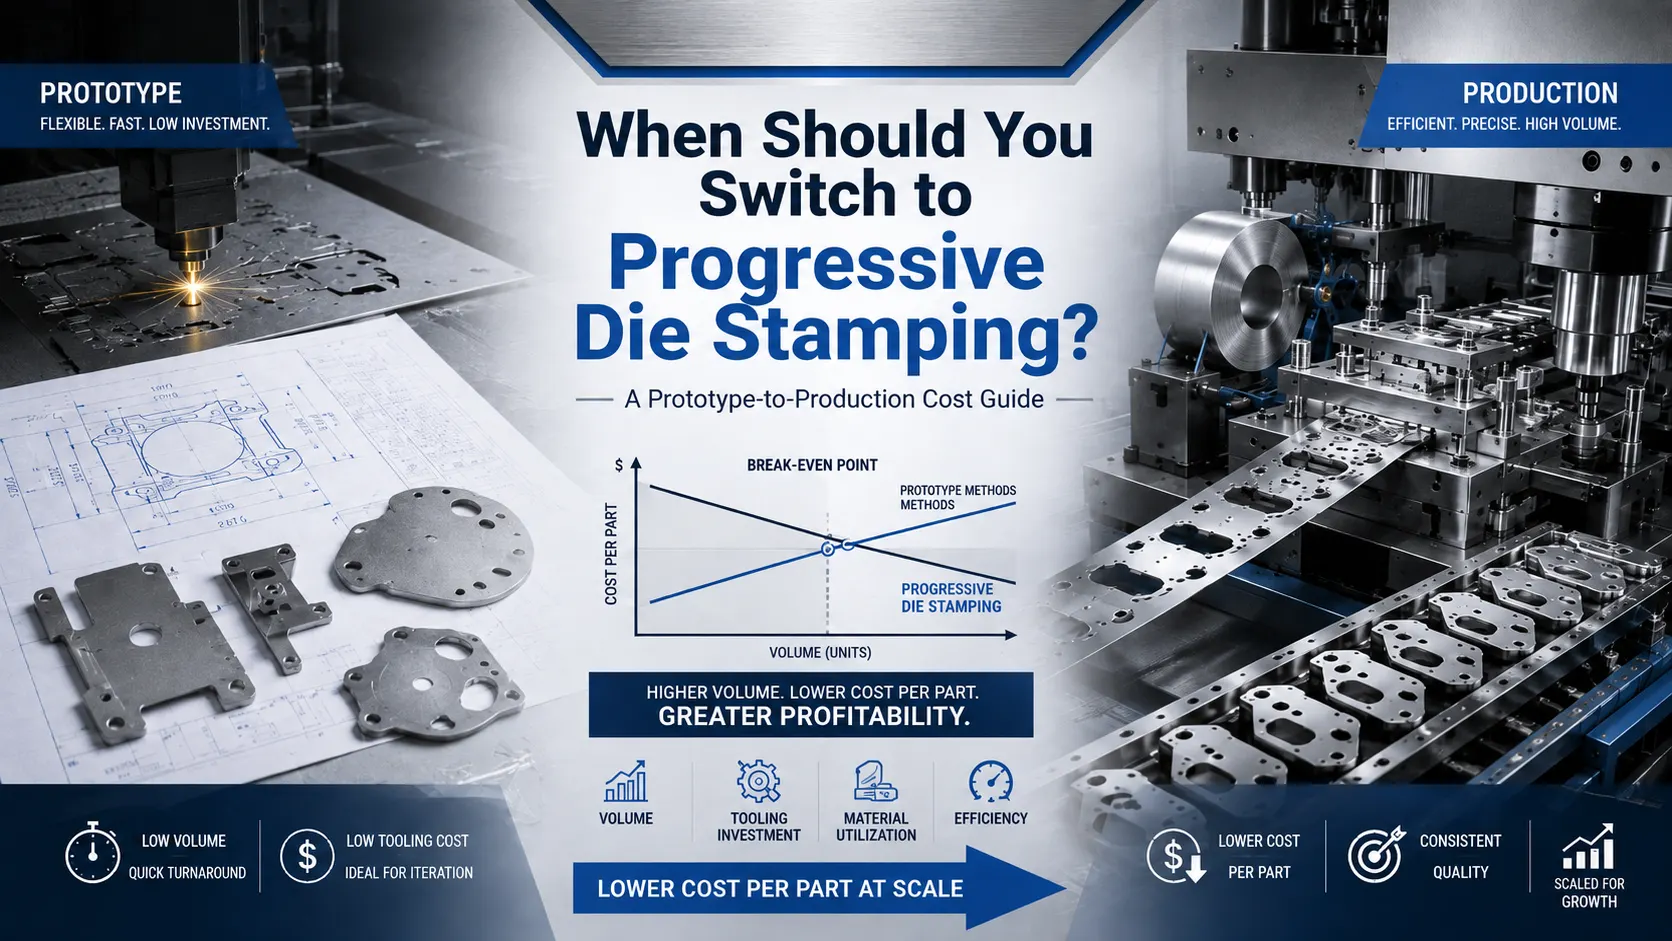
Switching from laser cutting or single-operation stamping to a progressive die is a production decision based on volume, geometry, material use, labor, and design stability. A progressive die stamping manufacturer can help compare these factors, but the buyer should understand the decision logic before requesting a quote.
The central question is not whether progressive stamping has a lower piece price. It is whether the tooling investment will reduce total lifecycle cost without creating excessive revision, quality, or maintenance risk.
Why Prototype-Friendly Processes Become Expensive in Production
Laser cutting and single-stage stamping are useful during prototyping because they require less dedicated tooling. They support frequent design changes and allow engineers to confirm fit, function, and assembly before the design is released.
Production introduces different cost drivers. Laser-cut parts may require separate bending, deburring, inspection, and handling. Single-operation stamping may involve several dies, manual transfers, repeated positioning, and additional work-in-process.
Hidden costs can include:
- Manual loading and unloading
- Multiple setups and die changes
- Repeated part location and measurement
- Handling between operations
- Material scrap from inefficient blanking
- Sorting, rework, and additional inspection
- Delays caused by inconsistent process flow
Laser cutting may remain suitable for low-volume work, frequent revisions, large flat profiles, or early prototypes. A dedicated die is less suitable when demand is uncertain or the design has not reached a meaningful freeze point.
When Should You Switch to Progressive Die Stamping?
Production Volume and Run Rate
There is no universal production quantity that justifies a progressive die. The decision depends on tooling cost, the difference between current and projected unit cost, and the expected lifetime demand.
A stable part with recurring releases is a stronger candidate than a part ordered only occasionally. Review annual volume, monthly release frequency, forecast reliability, and the expected production life. High volume metal stamping can produce attractive unit economics, but only when demand is sufficient to recover the initial tooling expense.
Request separate figures for:
- Die design and tooling
- Material and expected scrap
- Press operation
- Secondary operations
- Inspection and packaging
- Maintenance and replacement items
A combined price makes it difficult to calculate the actual break-even quantity.
Part Geometry, Operations, and Material Form
Progressive stamping generally fits parts produced from strip or coil through a sequence of blanking, piercing, bending, forming, and cutoff operations. Repeated features and a predictable feed direction make the process easier to evaluate.
The design review should cover:
- Number and sequence of operations
- Strip width and material utilization
- Hole-to-edge relationships
- Bend direction and forming access
- Flatness and positional requirements
- Burr direction and allowable edge condition
- Material grade and thickness
Parts with deep three-dimensional geometry, difficult forming behavior, or frequent design changes may require another process or a hybrid route. Material compatibility should be checked against the proposed progressive stamping dies and press setup. CK Metal Tech’s custom stamping tooling parts page can serve as a reference point when reviewing the range of components associated with stamping and tooling.
Design Stability and Revision Risk
Dedicated tooling should follow validation of critical interfaces and a reasonably stable design. A small hole-location change may require a limited modification, while a change to the part envelope, feed direction, or forming sequence can create more substantial rework.
A lower-risk transition is to use laser cutting or single-operation stamping during prototype and pilot builds, then release progressive tooling after the key dimensions have been verified. This approach helps prevent a die from being built before the production design is ready.
Progressive Stamping vs. Laser Cutting vs. Single-Stage Stamping
A meaningful comparison includes total cost, flexibility, and production risk.
| Decision factor | Laser cutting | Single-stage stamping | Progressive stamping |
|---|---|---|---|
| Design changes | Highly flexible | Moderate flexibility | Higher revision risk |
| Tooling investment | Low | Low to moderate | Higher upfront investment |
| Repetitive production | May become labor-intensive | May require multiple operations | Strong fit for stable repeat production |
| Material utilization | Depends on nesting | Depends on blank design | Depends on strip layout |
| Typical use | Prototypes and low volume | Small or medium repeat batches | Stable production with recurring demand |
| Main risk | Labor and cycle cost | Handling and setup cost | Tooling payback and maintenance |
Progressive metal stamping is not automatically the right choice for every high-volume part. Critical features may still require machining, secondary forming, or additional inspection. The most economical solution may combine processes instead of replacing every operation with one method.
How to Calculate Progressive Die Tooling Payback
Break-Even Quantity Formula
The basic calculation is:
Break-even quantity =
Tooling investment /
Existing unit cost – Progressive unit cost
For example, if tooling costs $24,000, the current process costs $1.20 per part, and the projected progressive process costs $0.70 per part:
$24,000 / ($1.20 – $0.70) = 48,000 parts
The tooling begins to recover its cost after approximately 48,000 parts, before maintenance, scrap variation, financing, and secondary operations are included.
The comparison should use equivalent quality requirements and include:
- Tool maintenance and spare components
- Setup and changeover time
- Scrap and rework
- Secondary forming or finishing
- Inspection labor
- Packaging and handling
- Expected engineering changes
This formula is a screening tool rather than a guaranteed financial result. Actual payback depends on the application and the assumptions used in the quotation.
Use Multiple Demand Scenarios
Calculate the payback period under conservative, expected, and high-demand forecasts. If the die only pays back under an optimistic scenario, retaining a flexible process may reduce commercial risk.
Repeat the calculation when material prices, part dimensions, release schedules, or annual demand change. A qualified progressive stamping supplier should identify which assumptions control the unit price and which figures remain provisional.
What to Validate Before Ordering a Progressive Die
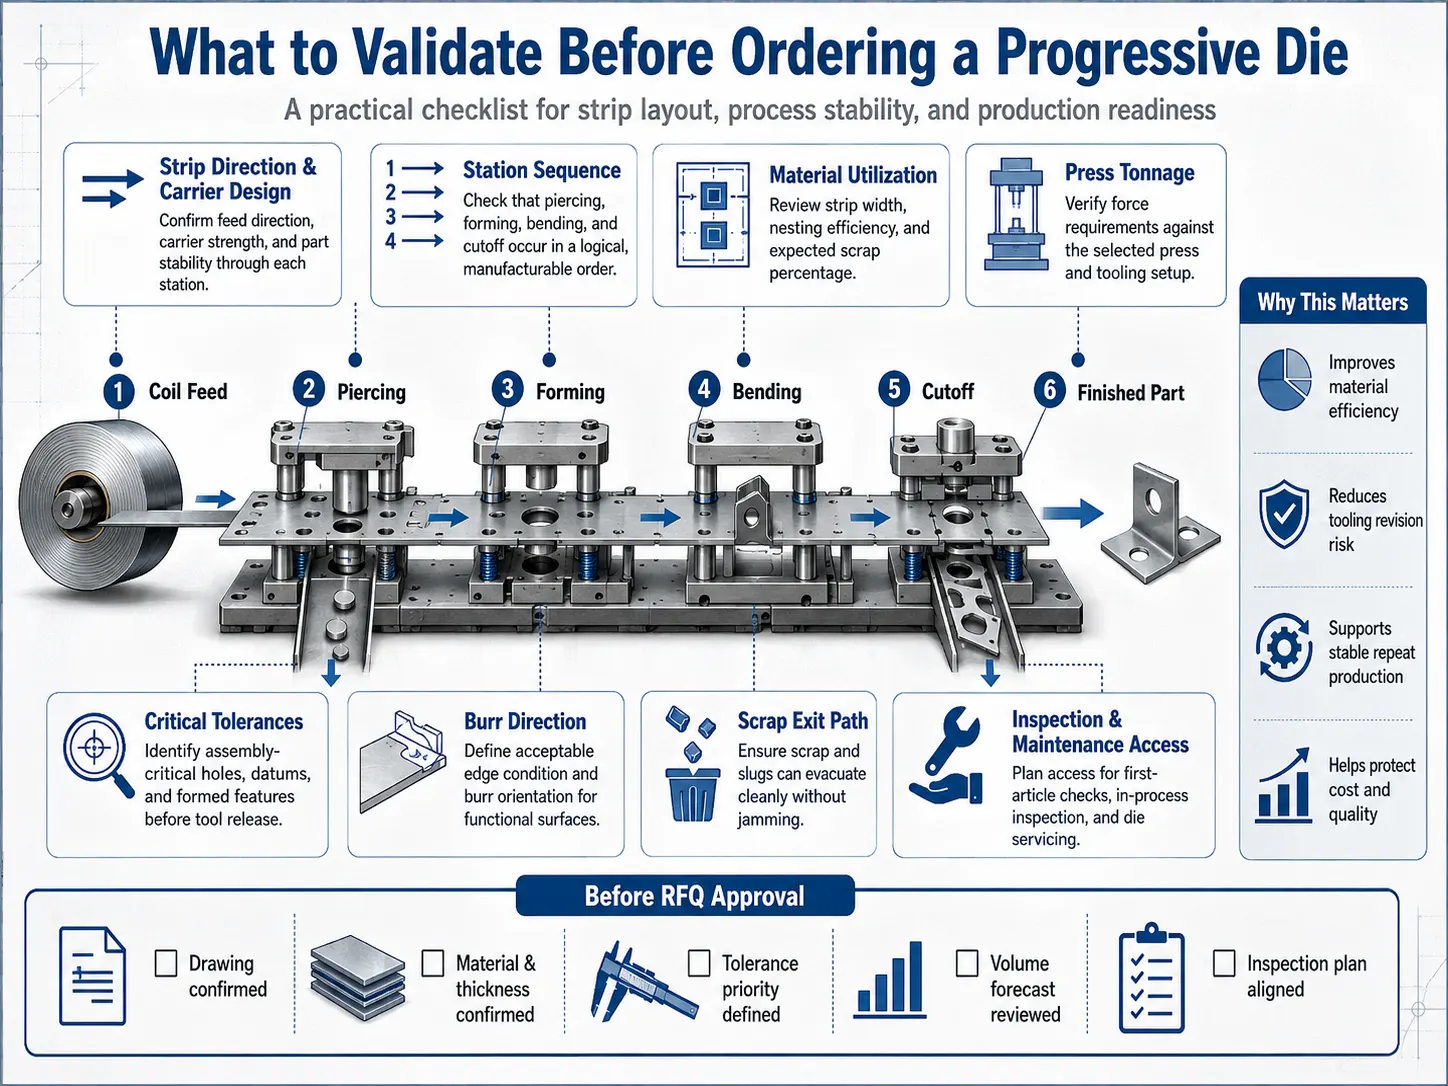
Strip Layout and Station Plan
The strip layout affects material utilization, station count, feed stability, and scrap removal. It should show how the part moves through piercing, forming, bending, and cutoff operations.
Before approval, request confirmation of:
- Strip direction and carrier design
- Station sequence
- Expected material utilization
- Scrap exit path
- Press tonnage requirement
- Access for inspection and maintenance
A documented station plan also helps purchasing compare custom progressive stamping quotations on the same technical basis.
Critical Tolerances, Burrs, and Formed Features
Not every dimension requires the same control level. Assembly-critical holes, datums, contact areas, and formed features should be identified before tooling release.
The supplier should clarify:
- Which dimensions are process-critical
- How burr direction will be controlled
- How springback or deformation will be checked
- What inspection method will be used
- How first-article approval will be documented
These checks reduce the risk of receiving parts that meet general dimensions but fail during assembly.
How to Choose a Progressive Die Stamping Manufacturer
A capable supplier should connect tooling design, die manufacturing, press production, inspection, and production support. Equipment alone does not demonstrate that a supplier can manage the transition from prototype to repeat production.
CK Metal Tech publicly describes integrated CNC machining, sheet metal, stamping, tooling, and assembly capabilities. Its website lists precision punch presses ranging from 16 to 250 tons, with a published maximum speed of 500 strokes per minute. Publicly listed material coverage includes brass, phosphor bronze, beryllium bronze, nickel white copper, steel, stainless steel, plated strip, galvanized sheet, and spring steel. Actual suitability still depends on the specific drawing, material, thickness, and process plan.
The tooling equipment category also identifies wire EDM and surface-grinding equipment. A related progressive die stamping terminal strip provides a relevant product reference for buyers assessing continuous stamping applications.
When comparing progressive stamping services, request:
- A drawing-based process review
- Proposed strip layout
- Separate tooling and piece-price quotations
- Material and thickness confirmation
- First-article and inspection plans
- Maintenance and spare-part expectations
- Clear assumptions behind the payback estimate
Conclusion
Progressive die stamping is worth evaluating when part geometry is stable, demand is recurring, multiple operations can be combined, and the expected lifecycle volume can recover the tooling investment. Laser cutting and single-operation stamping remain practical for prototypes, low-volume work, and designs that are still changing.
CK Metal Tech’s progressive die stamping and tooling services can be reviewed alongside the technical requirements for the part. For a project-specific assessment, submit the drawing, material, thickness, critical tolerances, target quantity, release schedule, and any available sample through request a stamping project review.
FAQs
What production volume justifies progressive die stamping?
No fixed quantity applies to every project. Calculate tooling investment divided by the unit-cost difference between the existing and progressive processes, then compare the result with realistic lifetime demand.
Is progressive stamping cheaper than laser cutting?
It may reduce unit cost for stable, repetitive production. Laser cutting can remain more practical for prototypes, low volumes, frequent revisions, or large flat parts.
How do you calculate progressive die payback?
Divide the tooling investment by the difference between the current unit cost and the projected progressive unit cost. Include maintenance, scrap, inspection, and secondary operations for a more useful estimate.
What should be included in a progressive stamping RFQ?
Include 2D and 3D drawings, material grade, thickness, annual quantity, release schedule, critical tolerances, surface requirements, inspection expectations, packaging, and samples when available.
How do you choose a progressive stamping supplier?
Compare die design, press capability, material experience, inspection planning, maintenance support, and the ability to manage tooling, tryout, first-article approval, and repeat production.
Leave a reply